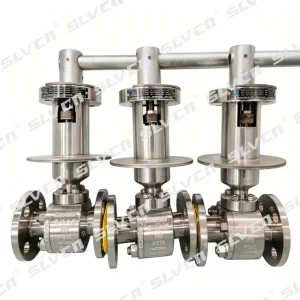
China has emerged as the global epicenter for industrial valve manufacturing, driven by a synthesis of advanced metallurgical research and rigorous adherence to international API, ASME, and ISO standards. For global procurement officers, the "China-factory" advantage goes beyond cost; it represents a mature supply chain integration that shortens lead times for complex, high-pressure, and cryogenic ball valves.
The transition toward Digitalized Valve Management—integrating smart actuators and predictive maintenance sensors—has placed Chinese manufacturers at the forefront of the "Industry 4.0" initiative. We observe a market shift where simple "on-off" utility is replaced by "Smart Isolation," emphasizing zero-leakage profiles, fire-safe certifications (API 607/6FA), and fugitive emission compliance.
Our valves are tailored for the unique challenges of the Middle Eastern desert heat and Arctic LNG environments, ensuring mechanical stability where standard valves often face fatigue.
From hydrogen storage high-pressure management to municipal water desalination, we provide integrated valve packages rather than isolated components.
ISO-certified manufacturing processes ensure that every batch, whether standard or bespoke OEM, meets the audit requirements of the most stringent global energy firms.
Chinese factories like ours leverage advanced CNC machining and strict third-party inspection protocols to deliver products that match or exceed Western European quality standards at significantly reduced lead times.
 Shoulong Valve