Explore our flagship OEM actuated valve solutions certified for high pressure, extreme temperature, and zero-leakage safety isolation.
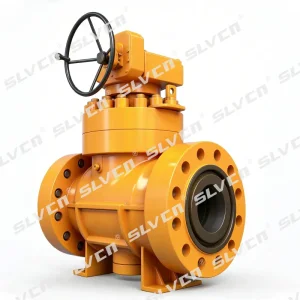
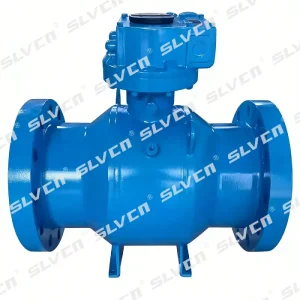
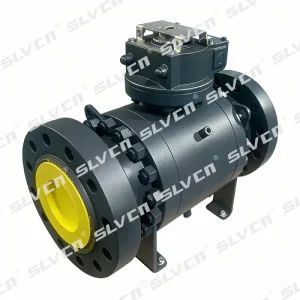
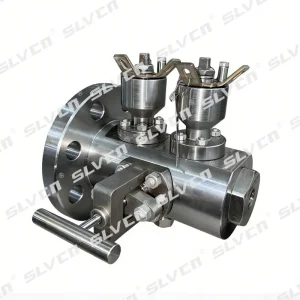
A Comprehensive Engineering Guide to Automated Process Control, Torque Optimization, and Zero-Fugitive Emission Performance.
In modern industrial process automation, the modern actuator control valve assembly serves as the critical final control element in process lines. Operating across severe-service sectors such as oil and gas refining, chemical synthesis, cryogenic LNG processing, and power generation, these engineered packages integrate precision mechanical valve bodies with sophisticated actuation systems. As a leading OEM Actuator Control Valve Manufacturer & Supplier, SLVCN engineers custom automated valve solutions designed to solve severe pressure drops, extreme thermal expansion, aggressive cavitation, and fugitive emission risks.
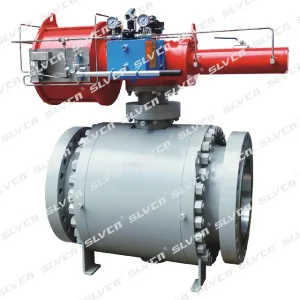
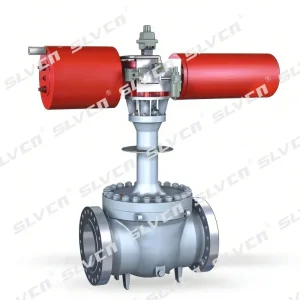
Pneumatic rack-and-pinion and scotch-yoke actuators provide high-speed emergency shutoff (ESD) capabilities, fail-safe spring returns, and continuous modulating control in explosive Class I, Div 1 zones.
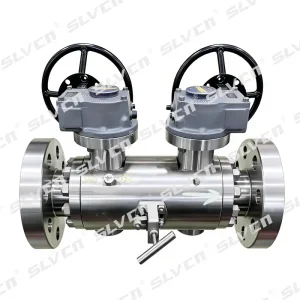
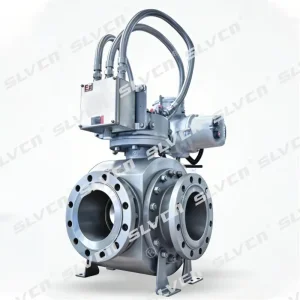
Non-intrusive smart electric actuators engineered with multi-turn or quarter-turn gearboxes, HART/Modbus digital feedback, and precise dynamic torque monitoring for automated DCS integration.
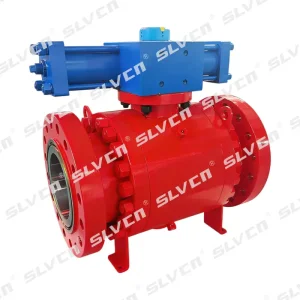
Engineered for high-thrust, heavy-torque applications such as subsea isolation and large-bore mainline transmission pipelines requiring immense holding torque and precise modulating speed.
Every SLVCN OEM actuated valve is manufactured with an ISO 5211 compliant top flange and heavy-duty drive stem. Our engineering protocol applies a minimum safety factor of 1.30 to 1.50 over maximum dynamic break-torque requirements, accounting for seat friction variations, media viscosity, and differential pressure build-up over years of continuous service.
Explore specialized valve engineering configurations tailored for severe operating conditions, trusted by mega-projects worldwide.
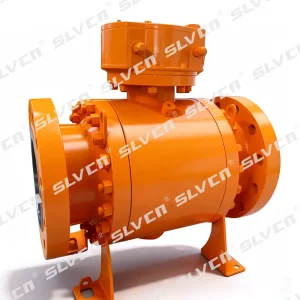
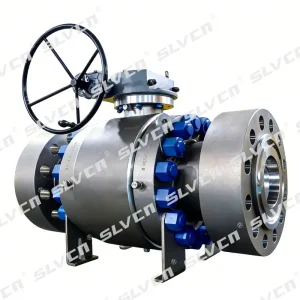
Engineered for Class 900–2500 service, utilizing forged A105, F316, or F11 body materials with metal-to-metal seating to achieve zero-leakage under extreme differential pressures up to 420 bar.
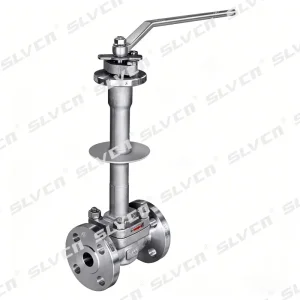
Designed with extended stems and vapor columns to maintain packing integrity at ultra-low operating temperatures down to -196°C in LNG liquefaction and liquid nitrogen plants.
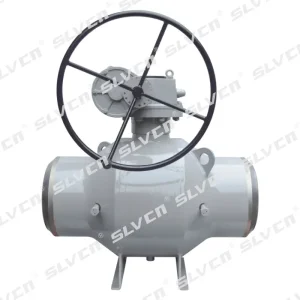
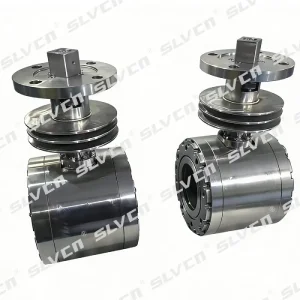
Eliminates external leak paths across body joints, ideal for high-pressure natural gas transmission lines and underground buried installations with extended maintenance-free lifespans.
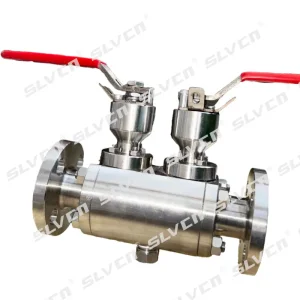
Features dual independent seating surfaces and a central cavity bleed valve to provide positive double isolation for instrument calibration and critical pipeline safety isolations.
Utilizes advanced surface hardening such as High-Velocity Oxygen Fuel (HVOF) Chrome Carbide or Stellite coatings, delivering rated performance up to +550°C in thermal power facilities.
Designed for inline maintenance without removing the valve body from the pipeline, significantly reducing system downtime in hazardous chemical processing units.
Engineered for Reliability Across High-Risk Critical Infrastructure & Industrial Applications.
Valves ensure strict pipeline isolation and safe operation across upstream extraction platforms, midstream compression stations, and downstream refineries under extreme fluid dynamics.
Engineered to maintain reliable micro-sealing integrity and stable long-term throttling control in highly corrosive media, thermal cycling, and polymerizing process fluids.
Delivering proven ultra-low temperature performance, bubble-tight sealing, and safe thermal expansion pressure management down to -196°C for cryogenic storage tanks and carriers.
Controls high-pressure steam, feed-water loops, and severe-service bypass systems operating in critical thermal and nuclear power generation units.
Provides robust corrosion-resistant isolation and precise throttling control in continuous, high-pressure reverse osmosis (SWRO) industrial operations.
Offers specialized high-integrity metallic sealing and fugitive emission stem packing designs to eliminate molecular hydrogen permeability and micro-leakage risks under elevated pressures.
Pioneering Next-Generation Autonomous Valve Control, Industrial IoT Integration, and Sustainability Innovations.
The landscape of industrial process control is undergoing a major shift driven by Industry 4.0 digitization, stringent environmental fugitive emission regulations, and the expansion of clean energy vectors like green hydrogen. As an innovative OEM Actuator Control Valve Manufacturer, SLVCN is at the forefront of this evolution, embedding advanced diagnostic and smart control technologies into our automated valve packages.
Next-generation actuated valves are equipped with intelligent digital positioners capable of real-time valve signature analysis. By continuously monitoring stem friction, dynamic packing wear, spring degradation, and seat seat leakage anomalies, our smart systems enable predictive maintenance before unexpected shut-downs occur.
Integrating WirelessHART and ISA100.11a communications, our smart electric and electro-hydraulic actuators enable remote valve health monitoring and control parameter adjustment in hard-to-reach offshore platforms and vast pipeline networks without costly control wiring infrastructure.
To combat climate change and reduce VOC emissions, our R&D team has engineered live-loaded PTFE and flexible graphite packing matrices paired with micro-finished stems (Ra < 0.2 µm). These designs guarantee leak rates under 10⁻⁵ mg/s·m, exceeding global environmental mandates.
Addressing the challenges of hydrogen embrittlement and high permeability, SLVCN is deploying specialized austenitic stainless steels, Inconel 718 stem designs, and metallic primary seals engineered to maintain tight shutoff up to 700 bar in hydrogen refueling and transport infrastructures.
Combining Advanced Automation, Rigorous Quality Control, and Unmatched Supply Chain Resilience.
Global engineering procurement managers face the dual challenge of ensuring uncompromising quality while optimizing capital expenditures (CAPEX). Leveraging China's premier industrial manufacturing ecosystem, SLVCN operates a state-of-the-art 10,000 m² facility equipped with multi-axis CNC machining centers, automated cladding stations, and specialized non-destructive testing (NDT) bays.
We source forged steel bodies (A105, F316, F22, Duplex 2205) exclusively from Tier-1 mills accompanied by EN 10204 3.1 chemical and mechanical test certificates, ensuring zero internal porosity or structural defects.
Spherical ball grinding tolerances within ±0.01 mm combined with automated Inconel 625 weld cladding on body sealing areas provide long-term resistance to aggressive sour gas (H₂S) corrosion.
Our vertically integrated supply chain enables rapid prototyping, custom face-to-face dimensions (ANSI B16.10 or non-standard), and fast-track production delivery cycles up to 40% shorter than traditional European manufacturers.
Every Valve Engineered and Tested in Strict Accordance with Recognized International Standards.
| Standard / Certification | Technical Scope | Operational Compliance Assurance |
|---|---|---|
| API 6D / ISO 14313 | Pipeline Valve Design & Specification | Guarantees full bore flow efficiency, DBB isolation capability, and standardized pressure testing protocols. |
| API 607 / ISO 10497 | Fire Test for Soft-Seated & Hard-Seated Valves | Ensures full sealing integrity during and after direct fire exposure up to 1000°C for hydrocarbon safety. |
| SIL 3 (IEC 61508) | Safety Integrity Level Automation | Validates low probability of failure on demand (PFD) for critical emergency shutdown (ESD) automated loops. |
| ISO 15848-1 & TA-Luft | Fugitive Emission Measurement | Certifies tight packing stem containment, eliminating hazardous chemical leakage into the ambient atmosphere. |
| NACE MR0175 / ISO 15156 | Sulfide Stress Cracking Resistant Materials | Mandates strict hardness control and heat treatment for severe sour gas (H₂S) process environments. |
| PED 2014/68/EU (CE Mark) | Pressure Equipment Directive Compliance | Permits seamless deployment and regulatory acceptance across European Union industrial markets. |
Key Considerations for Selecting the Ideal Actuator and Trim Design for Your Process Parameters.
Selecting an optimal OEM actuator control valve package requires rigorous engineering evaluation of system dynamics. Incorrect sizing can lead to control instability, rapid valve wear, high noise levels (>85 dBA), or severe cavitation damage. Our engineering support team assists global EPC buyers through a structured step-by-step sizing matrix:
Determining the exact required flow coefficient under maximum, normal, and minimum flow rates ensuring the control valve operates within its stable 20% to 80% opening stroke range to avoid seat erosion near shutoff.
For high differential pressure liquids ($\Delta P > 0.5 P_1$), SLVCN engineers multi-stage anti-cavitation trim sets that drop pressure incrementally, preventing fluid vaporization and micro-implosion damage to downstream piping.
Matching process control requirements with Equal Percentage, Linear, or Quick-Opening flow profiles to linearize the overall loop response relative to process system head loss curves.
Calculating peak breakaway torque, running torque, and end-of-stroke torque under maximum design differential pressure ($MOPD$), applying safe pneumatic spring margins for instant emergency fail-safe closure.
Engineered Valve Reliability for Critical Global Industrial Applications.
Quality and testing procedures applied in accordance with international standards for complete peace of mind.
100% Positive Material Identification (PMI) chemical verification and ultrasonic testing on all forged pressure-retaining bodies prior to machining.
Ultra-precise multi-axis CNC lathe turning and ball lapping guarantees spherical roundness, eliminating high friction and seat distortion.
Assembled in cleanrooms with torque-calibrated tooling to ensure packing compression and seat seal pre-load meet API 6D specifications.
Every single valve package undergoes 100% shell hydrostatic testing at 1.5× design pressure and seat gas testing per API 598 prior to shipment.
Stay informed with technical whitepapers and field deployment reports from our engineering team.
SLVCN is proud to announce the successful shipment of multiple 6" Class 300 RF forged trunnion-mounted ball valves equipped with heavy-duty pneumatic spring-return actuators for major offshore projects.
In high-stakes industries where safety and reliability are paramount—such as oil & gas and chemical processing—Double Block and Bleed valves provide verified dual boundary isolation.
With over 30 years of manufacturing experience, SLVCN continues to expand its technological capabilities in smart actuator integration, zero-emission stem seal matrices, and high-temp alloys.
Detailed Engineering Clarifications for OEM Valve Procurement, Actuator Sizing, and Field Operations.
Discover more specialized valve products available directly from our manufacturing facility.
 Shoulong Valve